

Views: 368 Author: Lasting titanium Publish Time: 2025-07-02 Origin: Site


Content Menu
● Introduction: The Significance of Titanium Bars
● Step 1: Titanium Ore Extraction and Refining
>> Mining and Beneficiation of Titanium Ore
>> The Kroll Process: Producing Titanium Sponge
● Step 2: Melting and Alloying
>> Alternative Melting Techniques
>> Ingot Formation and Quality Control
● Step 3: Primary Forming – Forging and Billet Production
>> Heating and Forging of Ingots
>> Hot Rolling
● Step 4: Precision Shaping – Rolling and Cold Drawing
>> Cold Drawing for High Precision
>> Annealing
>> Solution Treatment and Aging
● Applications of Titanium Bars
Titanium bars are essential materials in many high-performance industries, including aerospace, medical, marine, and chemical processing, due to their outstanding strength-to-weight ratio, corrosion resistance, and biocompatibility. The manufacturing process of titanium bars is complex and requires precise control at every stage to ensure the final product meets strict quality and performance standards. This article provides an in-depth exploration of the entire titanium bar production process, from raw ore extraction to the finished bar, detailing each step and its importance in producing high-quality titanium bars.
Titanium bars are widely used because of their exceptional mechanical properties and resistance to harsh environments. These bars form the foundation for critical components such as aircraft structural parts, surgical implants, and marine equipment. The production process must maintain the metal's purity and mechanical integrity to ensure reliability and safety in demanding applications. Understanding how titanium bars are made helps appreciate the sophisticated techniques and technologies involved in transforming raw materials into precision-engineered products.
Titanium does not occur naturally in its metallic form but is found in minerals such as rutile and ilmenite. Mining these ores typically involves open-pit methods, where large quantities of ore are extracted from the earth. The raw ore contains titanium dioxide along with impurities like iron, silica, and other minerals. To prepare the ore for further processing, it undergoes beneficiation—a series of crushing, washing, and separation steps that increase the titanium dioxide concentration and remove unwanted materials. This step is crucial for producing high-quality titanium feedstock.
The purified titanium dioxide is then chemically converted into metallic titanium sponge through the Kroll process, which remains the primary industrial method for titanium production. This multi-step chemical process involves:
- Chlorination: Titanium dioxide reacts with chlorine gas at elevated temperatures to form titanium tetrachloride (TiCl₄), a volatile liquid that can be purified by distillation.
- Reduction: Titanium tetrachloride is reduced by molten magnesium in an inert argon atmosphere, producing porous metallic titanium sponge and magnesium chloride as a byproduct.
The titanium sponge produced is a porous, brittle mass resembling a metallic foam. It is carefully inspected for purity and particle size, as these factors influence the quality of the final titanium bars. The sponge is the starting material for all titanium metal products, including bars.
To produce titanium bars with consistent composition and superior mechanical properties, the titanium sponge is melted and alloyed using Vacuum Arc Remelting (VAR). In this process:
- The titanium sponge is compressed into electrodes.
- These electrodes are melted under a high vacuum to prevent contamination from oxygen, nitrogen, or hydrogen, which can degrade the metal's properties.
- Alloying elements such as aluminum, vanadium, molybdenum, or molybdenum are added depending on the desired titanium grade, such as the widely used Ti-6Al-4V alloy.
- Multiple remelting cycles ensure chemical homogeneity and eliminate impurities.
VAR produces high-purity, defect-free titanium ingots essential for demanding applications like aerospace and medical implants.
For aerospace-grade titanium, additional melting techniques such as cold hearth melting using electron beam or plasma furnaces may be employed. These methods allow the removal of high-density inclusions and further improve purity and cleanliness of the titanium ingots.
The molten titanium alloy is cast into molds to form ingots, which can be cylindrical or rectangular blocks weighing several tons. Controlled cooling prevents internal defects such as cracks or porosity. After solidification, non-destructive testing methods, including ultrasonic inspections, verify the ingots' structural integrity before further processing.
The titanium ingots are reheated to temperatures typically between 900°C and 1100°C in protective atmospheres to prevent oxidation. At these temperatures, titanium becomes sufficiently ductile for forging.
Forging involves applying compressive forces using hydraulic presses or hammers to shape the ingots into blooms or billets. This step:
- Refines the internal grain structure, which enhances strength, toughness, and fatigue resistance.
- Breaks down coarse grains formed during casting.
- Shapes the material closer to the final bar dimensions, reducing waste in subsequent processes.
The forging process may involve multiple stages, including initial open-die forging followed by closed-die forging for precision shaping.
Following forging, billets are hot rolled to further reduce thickness and elongate the material, producing rough bars. Hot rolling improves the titanium's mechanical properties by aligning the grain flow and eliminating internal voids. Temperature and rolling speed are carefully controlled to avoid defects like cracking or warping.
The rough bars are passed through precision rolling mills to achieve the desired diameter and length. This step ensures uniform cross-sectional dimensions and improves surface finish. Rolling parameters such as temperature, reduction ratio, and roll speed are optimized based on the titanium grade and bar specifications.
For applications requiring tight dimensional tolerances and superior surface quality, titanium bars undergo cold drawing. This process involves:
- Cleaning the bar surface by acid pickling to remove oxide layers and contaminants.
- Applying lubricants to reduce friction during drawing.
- Pulling the bar through progressively smaller dies to reduce diameter and improve surface finish.
Cold drawing increases the bar's strength through work hardening and achieves dimensional tolerances as tight as ±0.05 mm, which is critical for medical implants and aerospace components.
Heat treatment processes are applied to tailor the mechanical properties of titanium bars according to their intended use.
Annealing involves heating the bars to moderate temperatures (650°C to 760°C) followed by slow cooling. This process:
- Relieves internal stresses induced by cold working.
- Improves ductility and toughness.
- Reduces brittleness, making the bars easier to machine and form.
Certain titanium alloys, especially Ti-6Al-4V, undergo solution treatment and aging to enhance strength and corrosion resistance. Solution treatment heats the bars above the beta-transus temperature, followed by rapid cooling to retain a metastable microstructure. Aging then precipitates fine particles that strengthen the alloy.
The final surface condition of titanium bars is crucial for performance, especially in medical and aerospace applications.
Bars are polished or ground to achieve smooth, defect-free surfaces that reduce friction and improve fatigue resistance. For medical implants, surface roughness is minimized to promote osseointegration and reduce bacterial adhesion.
In some cases, bars receive anodizing treatments to increase corrosion resistance or provide color coding for identification. Other coatings may be applied to enhance wear resistance or biocompatibility.
Additional machining processes such as CNC milling, turning, or threading are performed to create features like grooves, threads, or complex geometries required by specific applications.
Throughout the manufacturing process, titanium bars undergo stringent quality control to ensure compliance with industry standards.
- Chemical Composition Analysis: Confirms alloying elements are within specified ranges.
- Mechanical Testing: Tensile strength, hardness, fatigue, and impact tests verify mechanical performance.
- Non-Destructive Testing: Ultrasonic, magnetic particle, dye penetrant, and radiographic tests detect internal and surface defects.
- Dimensional Inspection: Ensures bars meet precise size and shape tolerances.
These controls guarantee that titanium bars are reliable and suitable for critical applications.
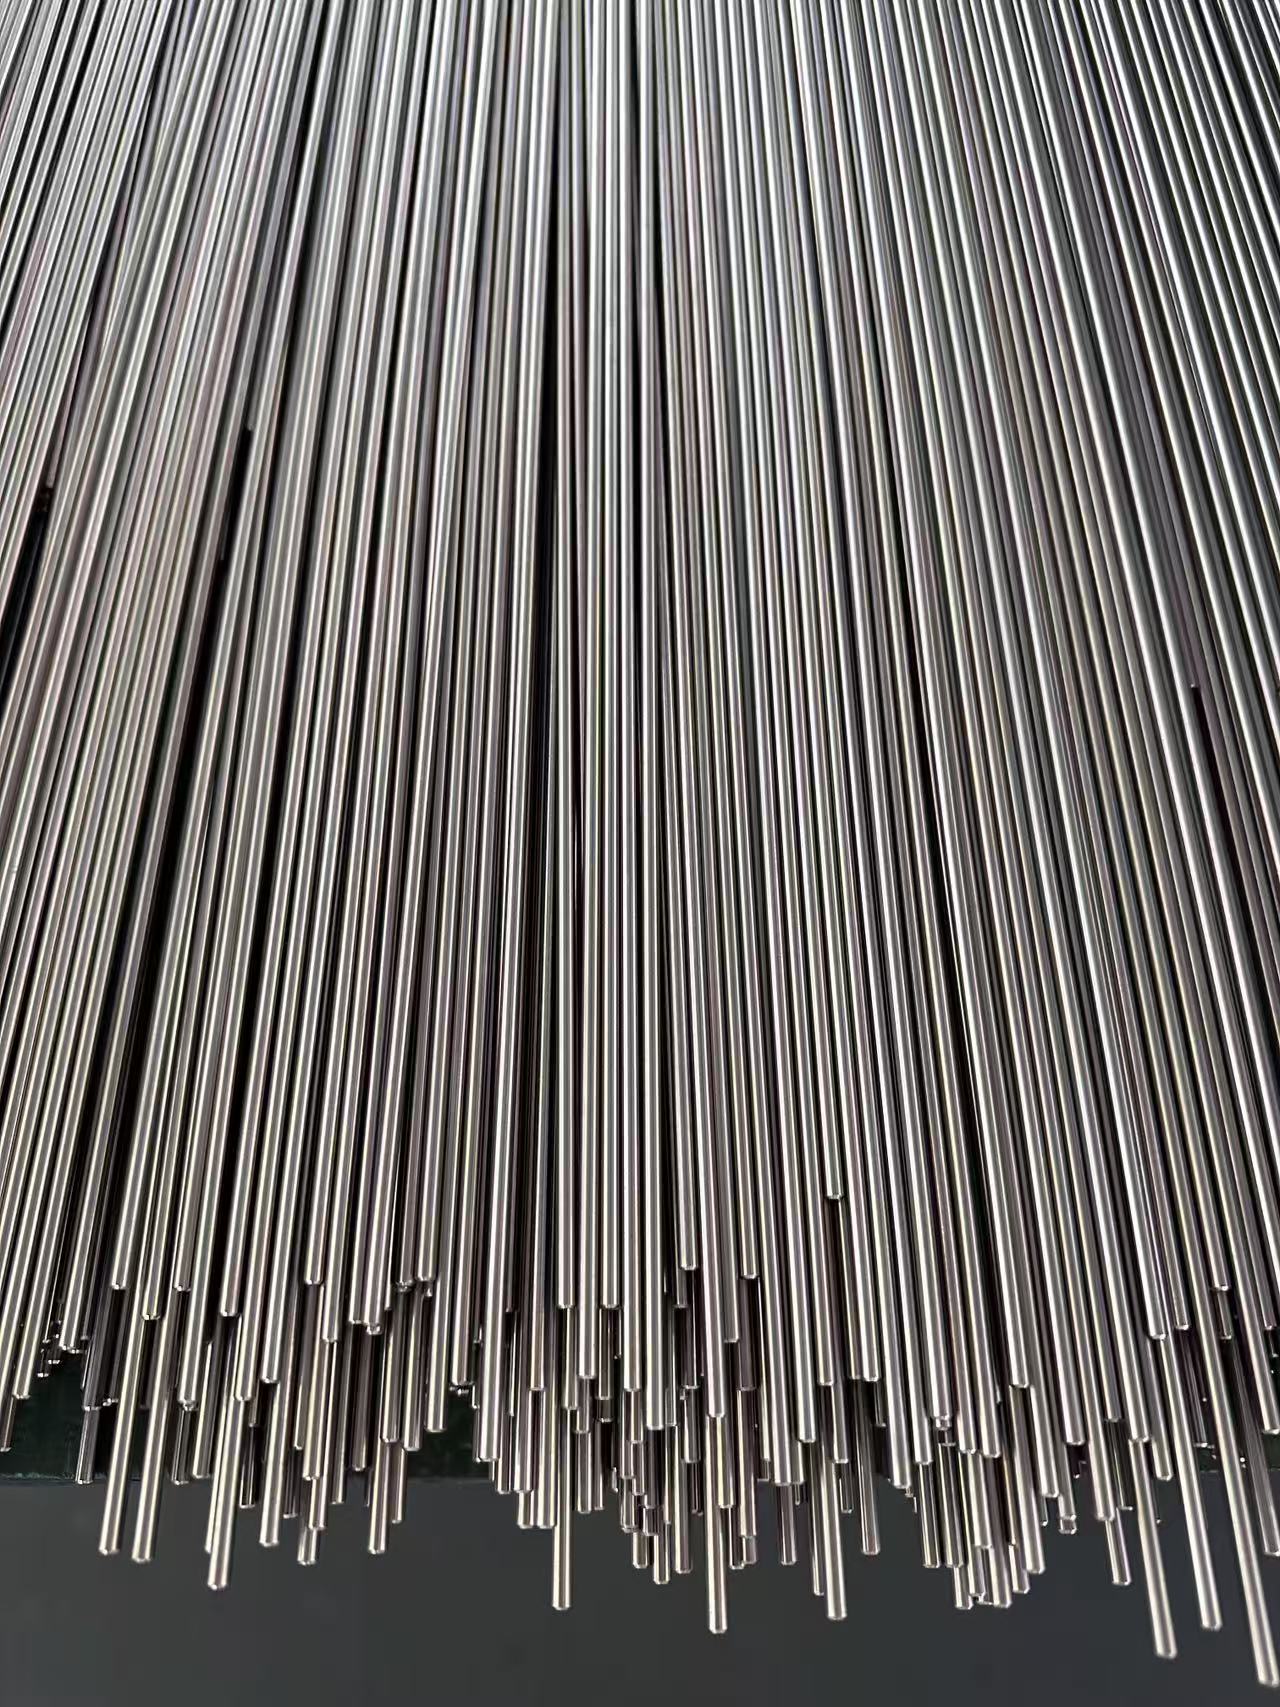
Titanium bars produced through this meticulous process find applications in:
- Aerospace: Structural components, engine parts, fasteners.
- Medical Devices: Orthopedic implants, dental implants, surgical instruments.
- Marine Industry: Shipbuilding, offshore platforms, desalination equipment.
- Chemical Processing: Heat exchangers, reactors, piping.
- Sports Equipment and Automotive: Lightweight, strong components.
The superior properties of titanium bars make them indispensable in these demanding fields.
Q1: Why is the Kroll process essential in titanium bar production?
A1: The Kroll process converts titanium ore into titanium sponge, the fundamental raw material for titanium metal production, through a controlled chemical reduction that ensures high purity.
Q2: What role does Vacuum Arc Remelting (VAR) play in titanium manufacturing?
A2: VAR refines titanium sponge electrodes under vacuum, removing impurities and ensuring chemical homogeneity, which is critical for high-performance titanium alloys.
Q3: How does forging improve titanium bar properties?
A3: Forging refines the grain structure, enhances mechanical properties, and shapes the metal closer to final dimensions, reducing defects and improving strength.
Q4: Why is cold drawing necessary for some titanium bars?
A4: Cold drawing achieves precise dimensions, improves surface finish, and increases strength through work hardening, essential for applications like medical implants.
Q5: What types of heat treatments are applied to titanium bars?
A5: Annealing relieves stresses and improves ductility, while solution treatment and aging enhance strength and corrosion resistance, tailored to specific alloys.


