

Views: 380 Author: Lasting Titanium Publish Time: 2025-05-02 Origin: Site


Content Menu
● Introduction to Titanium Reducers
● 1. Exceptional Corrosion Resistance
>> 1.1 The Role of the Oxide Layer
● 2. High Strength-to-Weight Ratio
>> 2.1 Implications for Design and Efficiency
>> 3.1 Performance Under Stress
>> 4.1 Implications for Chemical Processing
● 5. Long-Term Cost Effectiveness
● 6. Versatility in Applications
● 7. Environmental Considerations
>> 7.1 Sustainability in Chemical Processing
>> 1. What are titanium reducers used for in chemical processing?
>> 2. Why is titanium preferred over other metals for reducers?
>> 3. How does the oxide layer on titanium enhance its performance?
>> 4. Are titanium reducers cost-effective in the long run?
>> 5. Can titanium reducers be recycled?
Titanium has emerged as a leading material in the construction of reducers used in chemical processing plants. Its unique properties make it an ideal choice for applications where durability, corrosion resistance, and strength are paramount. This article explores the reasons why titanium is the best choice for reducers, particularly in the demanding environments of chemical processing.
Reducers are essential components in piping systems, designed to connect pipes of different diameters. In chemical processing plants, where the flow of various substances is critical, the choice of material for these reducers can significantly impact the efficiency and safety of operations. Titanium reducers are increasingly favored due to their exceptional characteristics. The importance of selecting the right material cannot be overstated, as it directly influences the longevity and reliability of the entire piping system. As industries evolve and face new challenges, titanium stands out as a material that meets the rigorous demands of modern chemical processing.
One of the most significant advantages of titanium is its outstanding corrosion resistance. In chemical processing environments, equipment is often exposed to aggressive substances that can lead to rapid degradation. Titanium forms a stable, protective oxide layer that prevents corrosion, making it suitable for handling corrosive chemicals such as acids and chlorides. This property ensures that titanium reducers maintain their integrity over time, reducing the need for frequent replacements and maintenance. The ability to withstand harsh environments without succumbing to corrosion not only extends the lifespan of the reducers but also enhances the overall safety of the chemical processing operations.
The natural formation of a continuous and adherent oxide film on titanium surfaces is crucial. This passive layer not only protects the metal from corrosive agents but also reforms quickly if damaged. This self-healing capability is particularly beneficial in environments where mechanical wear and tear are common. The oxide layer acts as a barrier, preventing the underlying metal from coming into contact with corrosive substances. This characteristic is especially important in applications where the reducers are subjected to fluctuating temperatures and pressures, as it ensures consistent performance and reliability.
Titanium is known for its remarkable strength-to-weight ratio. It is significantly lighter than many other metals, such as steel, while still providing comparable or superior strength. This characteristic is particularly advantageous in chemical processing plants, where reducing the weight of equipment can lead to easier handling and installation. The lightweight nature of titanium allows for more efficient designs in piping systems, enabling engineers to create configurations that are not only easier to install but also require less structural support.
The lightweight nature of titanium reducers allows for more efficient designs in piping systems. Engineers can create systems that are easier to install and maintain, ultimately leading to lower operational costs. Additionally, the reduced weight can lead to savings in structural support requirements, further enhancing the overall efficiency of the plant. This aspect is particularly beneficial in retrofitting existing systems, where the addition of lighter materials can improve the overall performance without the need for extensive modifications.
In many chemical processing applications, equipment is subjected to extreme temperatures. Titanium exhibits excellent thermal stability, maintaining its mechanical properties even at elevated temperatures. This stability is crucial for reducers that may experience significant temperature fluctuations during operation. The ability of titanium to withstand high temperatures without losing strength makes it an ideal choice for reducers in applications such as reactors and heat exchangers.
The ability of titanium to withstand high temperatures without losing strength makes it an ideal choice for reducers in applications such as reactors and heat exchangers. This performance under stress ensures that the reducers can handle the thermal expansion and contraction that occurs during chemical reactions. Moreover, titanium's thermal conductivity allows for efficient heat transfer, which is essential in processes where temperature control is critical. This characteristic not only enhances the efficiency of the chemical reactions but also contributes to the overall safety of the operations.
In addition to its corrosion resistance, titanium is also less prone to biofouling compared to other materials. Biofouling occurs when microorganisms attach to surfaces, leading to blockages and reduced efficiency in piping systems. The smooth surface of titanium reducers makes it difficult for organisms to adhere, thereby minimizing maintenance issues related to fouling. This property is particularly important in chemical processing plants that handle organic materials or operate in marine environments.
The reduced risk of biofouling is particularly important in chemical processing plants that handle organic materials or operate in marine environments. By choosing titanium reducers, operators can ensure a more reliable and efficient flow of materials, reducing downtime and maintenance costs. This reliability is crucial for maintaining production schedules and ensuring the safety of the operations. Furthermore, the reduced need for chemical cleaning agents to combat biofouling contributes to a more environmentally friendly operation.
While titanium may have a higher initial cost compared to other materials, its long-term benefits often outweigh these expenses. The durability and corrosion resistance of titanium reducers lead to lower maintenance and replacement costs over time. Additionally, the efficiency gains from using lightweight and thermally stable materials can result in significant operational savings. This financial aspect is critical for chemical processing plants that operate on tight margins and require reliable performance from their equipment.
Investing in titanium reducers can be seen as a long-term strategy for chemical processing plants. The initial investment is offset by the reduced need for repairs and replacements, as well as the enhanced efficiency of operations. This makes titanium a financially sound choice for many applications. Moreover, as the industry continues to evolve towards more sustainable practices, the long lifespan and recyclability of titanium further enhance its appeal as a responsible investment.
Titanium reducers are versatile and can be used in a wide range of applications within the chemical processing industry. They are commonly found in reactors, storage tanks, and pipelines, where they connect different pipe sizes and ensure the smooth flow of materials. This versatility allows for the integration of titanium reducers into various systems, enhancing their overall functionality.
- Chemical Reactors: Titanium reducers are used to connect pipes of varying diameters in reactors, ensuring efficient flow and minimizing pressure drops. Their ability to withstand high pressures and temperatures makes them ideal for this application.
- Storage Tanks: In storage tanks, titanium reducers help manage the flow of chemicals, preventing leaks and ensuring safety. Their corrosion resistance is particularly beneficial in environments where chemicals are stored for extended periods.
- Pipelines: Titanium reducers are essential in pipelines that transport corrosive substances, providing a reliable connection that withstands harsh conditions. Their lightweight nature also facilitates easier installation and maintenance in complex piping systems.
As industries move towards more sustainable practices, the choice of materials becomes increasingly important. Titanium is a highly recyclable material, making it an environmentally friendly option for reducers in chemical processing plants. The ability to recycle titanium reduces waste and conserves resources, aligning with the goals of many modern chemical processing operations.
By choosing titanium reducers, chemical processing plants can contribute to sustainability efforts while maintaining high operational standards. The long lifespan and recyclability of titanium make it a responsible choice for environmentally conscious companies. Additionally, the reduced need for chemical treatments and maintenance associated with titanium's resistance to corrosion and biofouling further supports sustainable practices in the industry.
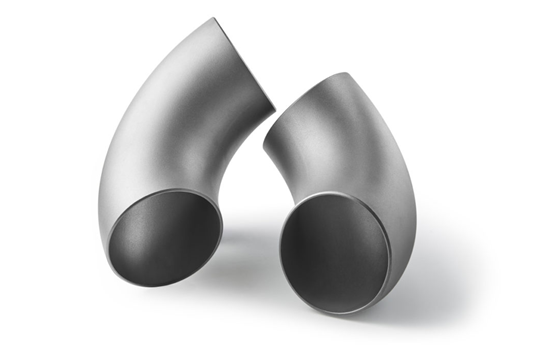
In conclusion, titanium stands out as the best choice for reducers in chemical processing plants due to its exceptional corrosion resistance, high strength-to-weight ratio, thermal stability, resistance to biofouling, long-term cost-effectiveness, versatility, and environmental benefits. As the chemical industry continues to evolve, the adoption of titanium reducers is likely to increase, driven by the need for safer, more efficient, and environmentally friendly solutions. The combination of these factors positions titanium as a material that not only meets the current demands of the industry but also paves the way for future advancements in chemical processing technology.
Titanium reducers are used to connect pipes of different diameters in chemical processing systems, ensuring efficient flow and minimizing pressure drops. Their unique properties make them suitable for handling a wide range of chemicals.
Titanium is preferred due to its outstanding corrosion resistance, high strength-to-weight ratio, and thermal stability, making it ideal for harsh chemical environments. These characteristics ensure reliability and longevity in demanding applications.
The oxide layer on titanium provides a protective barrier against corrosion and can quickly reform if damaged, ensuring long-lasting durability in aggressive environments. This self-healing property is crucial for maintaining the integrity of the reducers.
Yes, while titanium reducers may have a higher initial cost, their durability and low maintenance needs often lead to significant long-term savings. The investment in titanium is justified by the reduced need for repairs and replacements.
Yes, titanium is highly recyclable, making it an environmentally friendly choice for chemical processing applications. This recyclability contributes to sustainability efforts within the industry.


