

Views: 356 Author: Lasting Titanium Publish Time: 2025-04-08 Origin: Site


Content Menu
● 1. Chemical Processing Equipment
>> Overview
>> Benefits
>> Overview
>> Benefits
>> Overview
>> Benefits
● 4. Pharmaceutical Manufacturing
>> Overview
>> Benefits
>> Overview
>> Benefits
>> 1. What are titanium reducers?
>> 2. Why are titanium reducers preferred in the chemical industry?
>> 3. Can titanium reducers be used in high-temperature applications?
>> 4. How do titanium reducers compare to stainless steel reducers?
>> 5. What industries benefit from using titanium reducers?
Titanium reducers are essential components in the chemical industry, known for their exceptional strength, lightweight nature, and remarkable resistance to corrosion. These properties make titanium reducers ideal for various applications, particularly in environments where aggressive chemicals are handled. In this article, we will explore the top five applications of titanium reducers in the chemical industry, highlighting their significance and advantages.
Titanium reducers are widely used in chemical processing equipment due to their ability to withstand harsh environments. They are commonly found in reactors, storage tanks, and pipelines where aggressive chemicals are present. The chemical processing industry often involves the handling of corrosive substances, which can lead to equipment degradation over time. Titanium's unique properties make it a preferred material for constructing reducers that connect different pipe sizes, ensuring seamless flow and minimizing the risk of leaks.
- Corrosion Resistance: Titanium's resistance to corrosion ensures the integrity of the equipment, reducing the risk of leaks and failures. This is particularly important in chemical processing, where even minor leaks can lead to significant safety hazards and environmental concerns.
- Longevity: The durability of titanium leads to a longer lifespan for equipment, minimizing the need for frequent replacements and lowering maintenance costs. This longevity translates into reduced downtime for operations, allowing companies to maintain productivity and efficiency.
- Safety: Using titanium reducers enhances safety in chemical processing by preventing leaks and ensuring reliable operation under extreme conditions. The ability to withstand high pressures and temperatures without compromising structural integrity is crucial in maintaining safe operational environments.
The chlor-alkali industry is one of the first sectors to utilize titanium in chemical applications. Titanium reducers play a crucial role in the production of chlorine, caustic soda, and other chemicals. This industry is vital for producing essential chemicals used in various applications, including water treatment, paper manufacturing, and the production of plastics. The use of titanium in this sector has revolutionized the way these chemicals are produced, enhancing efficiency and safety.
- High Chemical Resistance: Titanium can withstand exposure to chlorine and other corrosive substances, making it ideal for use in chlor-alkali plants. This resistance helps prevent equipment failure and extends the operational life of processing equipment.
- Efficiency: The use of titanium reducers in this industry improves the efficiency of chemical reactions and processes, leading to higher productivity. By facilitating smoother flow and reducing friction, titanium reducers contribute to optimized production rates.
- Environmental Protection: By preventing leaks and failures, titanium reducers help minimize environmental pollution associated with chemical production. This is increasingly important as industries face stricter regulations regarding environmental impact and sustainability.
In the oil and gas sector, titanium reducers are used in various applications, including pipelines and offshore platforms. Their lightweight nature and strength make them suitable for demanding environments. The oil and gas industry often operates in challenging conditions, including extreme temperatures and corrosive environments, making the choice of materials critical for operational success.
- Weight Reduction: Titanium reducers are significantly lighter than steel, which reduces the overall weight of piping systems and structures. This weight reduction is particularly beneficial in offshore applications, where minimizing weight can lead to cost savings in transportation and installation.
- Resistance to Corrosion: The ability of titanium to resist corrosion from saltwater and other harsh chemicals is crucial in offshore applications. This resistance helps ensure the reliability of pipelines and equipment, reducing the risk of leaks and failures that can have catastrophic consequences.
- Enhanced Performance: The use of titanium reducers contributes to the overall performance and reliability of oil and gas operations. By maintaining structural integrity under extreme conditions, titanium reducers help ensure continuous operation and reduce the likelihood of costly downtime.

The pharmaceutical industry requires high standards of cleanliness and safety in its manufacturing processes. Titanium reducers are increasingly used in this sector due to their non-reactive nature. In pharmaceutical manufacturing, the integrity of the product is paramount, and the materials used in production must not contaminate the final product. Titanium's inert properties make it an ideal choice for this sensitive industry.
- Non-Reactivity: Titanium does not react with most chemicals, making it suitable for handling sensitive pharmaceutical compounds. This non-reactivity ensures that the purity of the products is maintained throughout the manufacturing process.
- Sterilization: Titanium reducers can withstand high temperatures and pressures, allowing for effective sterilization processes. This capability is essential in ensuring that equipment is free from contaminants before it comes into contact with pharmaceutical products.
- Quality Assurance: The use of titanium in pharmaceutical manufacturing helps ensure the quality and safety of the final products. By minimizing the risk of contamination and equipment failure, titanium reducers contribute to the overall reliability of pharmaceutical production.
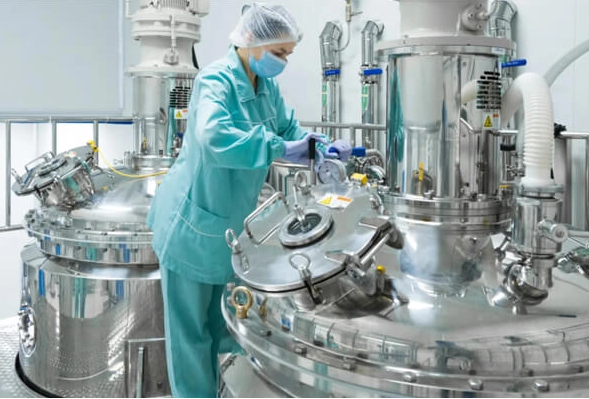
Titanium reducers are also employed in wastewater treatment facilities, where they are used in various applications, including piping and treatment tanks. The treatment of wastewater is critical for environmental protection and public health, and the materials used in these processes must be durable and reliable. Titanium's properties make it an excellent choice for this application, as it can withstand the harsh conditions often found in wastewater treatment.
- Durability: The corrosion resistance of titanium ensures that equipment remains functional and reliable over time, even in harsh wastewater environments. This durability is essential for maintaining continuous operation and meeting regulatory standards.
- Cost-Effectiveness: The longevity of titanium reducers reduces the need for frequent replacements, leading to lower operational costs. By minimizing maintenance and replacement expenses, facilities can allocate resources more effectively.
- Environmental Compliance: Using titanium in wastewater treatment helps facilities meet environmental regulations by minimizing the risk of leaks and contamination. This compliance is increasingly important as regulatory bodies impose stricter standards on wastewater management.
Titanium reducers are invaluable in the chemical industry, offering numerous advantages such as corrosion resistance, durability, and safety. Their applications span various sectors, including chemical processing, chlor-alkali production, oil and gas, pharmaceuticals, and wastewater treatment. As industries continue to seek materials that enhance performance and reduce environmental impact, the use of titanium reducers is expected to grow. The ongoing advancements in titanium technology and manufacturing processes will likely lead to even more innovative applications in the future.
- Titanium reducers are fittings used to connect pipes of different diameters, made from titanium, known for their strength and corrosion resistance.
- They are preferred due to their exceptional resistance to corrosion, lightweight nature, and ability to withstand harsh chemical environments.
- Yes, titanium reducers can withstand high temperatures, making them suitable for various industrial applications, including chemical processing and oil and gas.
- Titanium reducers offer better corrosion resistance and a higher strength-to-weight ratio compared to stainless steel, making them more suitable for aggressive chemical environments.
- Industries such as chemical processing, oil and gas, pharmaceuticals, and wastewater treatment benefit significantly from the use of titanium reducers.


