

Views: 368 Author: Lasting Titanium Publish Time: 2024-10-12 Origin: Site


Content Menu
● Introduction to Titanium Forging
● Understanding Titanium and Its Alloys
>> Common Titanium Alloys Used in Forging
● The Titanium Forging Process: Step by Step
>> Lubrication
● Advanced Techniques in Titanium Forging
● Applications of Titanium Forged Components
● Future Trends in Titanium Forging
>> Additive Manufacturing Integration
>> Advanced Simulation and Modeling
Titanium forging is a critical manufacturing process that has revolutionized various industries, particularly aerospace, automotive, and medical sectors. This sophisticated technique involves shaping titanium alloys into high-strength, corrosion-resistant, and heat-resistant components. The titanium forging process is essential for producing parts that require exceptional performance under extreme conditions. In this comprehensive guide, we will delve into the intricacies of the titanium forging process, exploring its various stages, benefits, and applications.
Titanium is a remarkable metal known for its exceptional strength-to-weight ratio, corrosion resistance, and biocompatibility. These properties make it an ideal material for a wide range of applications, from aerospace components to medical implants. However, working with titanium presents unique challenges due to its high melting point and reactivity at elevated temperatures.
Several titanium alloys are commonly used in the forging process, each with specific characteristics suited for different applications. The most widely used alloy is Ti-6Al-4V, which offers an excellent balance of strength, ductility, and machinability. Other popular alloys include Ti-6246 and Ti-5553, which are often chosen for their superior strength and heat resistance properties.
The titanium forging process begins with careful billet preparation. A billet is a solid, cylindrical piece of titanium alloy that serves as the starting material for forging. The quality of the billet is crucial, as any imperfections can lead to defects in the final product. The billet is typically prepared through a series of steps, including melting, casting, and initial shaping.
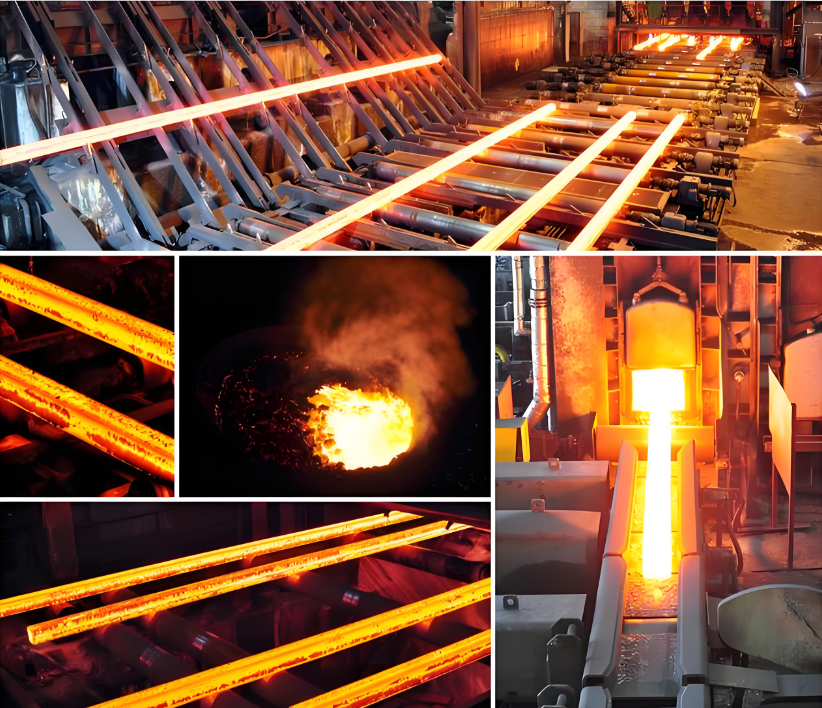
Once the billet is prepared, it must be heated to the appropriate forging temperature. This step is critical, as the temperature directly affects the material's formability and the resulting microstructure. For most titanium alloys, the forging temperature ranges between 870°C and 980°C (1600°F to 1800°F). Precise temperature control is essential to achieve the desired properties in the finished product.
Before the actual forging process begins, the heated billet and forging dies are coated with a lubricant. This step is crucial for reducing friction between the titanium and the die surfaces, preventing sticking, and ensuring smooth material flow during forging. The choice of lubricant depends on factors such as the specific alloy being forged and the forging temperature.
The core of the titanium forging process involves applying controlled pressure to the heated billet using specialized forging equipment. This can be done through various methods, including open-die forging, closed-die forging, and isothermal forging. Each method has its advantages and is chosen based on the desired final shape, size, and properties of the component.
Open-Die Forging
In open-die forging, the titanium billet is compressed between two flat or simply shaped dies. This method is often used for producing large, simple shapes or as a preliminary step before more complex forging operations. Open-die forging allows for greater control over the grain structure and can help improve the material's mechanical properties.
Closed-Die Forging
Closed-die forging involves shaping the titanium billet within a set of dies that contain a cavity in the shape of the desired final product. This method is ideal for producing complex shapes with high precision and consistency. Closed-die forging can be further categorized into impression-die forging and flash forging, depending on whether excess material is allowed to escape from the die cavity.
Isothermal Forging
Isothermal forging is an advanced technique where both the titanium workpiece and the forging dies are heated to the same temperature. This method allows for more precise control over the material flow and resulting microstructure. Isothermal forging is particularly useful for producing components with intricate geometries and tight tolerances, such as aircraft engine parts.
Post-Forging Operations
After the primary forging process, several post-forging operations are typically performed to enhance the properties and finish of the titanium component.
Cleaning
The forged titanium part undergoes a thorough cleaning process to remove any residual lubricant, scale, or other contaminants from its surface. This step is crucial for ensuring the quality and integrity of the final product.
Heat Treatment
Heat treatment is often performed on forged titanium components to optimize their mechanical properties. This process can involve various techniques such as solution treating, aging, or stress relieving, depending on the specific alloy and desired characteristics.
Machining and Finishing
Many forged titanium components require additional machining to achieve their final dimensions and surface finish. This may include operations such as turning, milling, grinding, or polishing. The choice of machining techniques depends on the component's geometry and the required tolerances.
Beta processing is a specialized forging technique used for certain titanium alloys, particularly Ti-6246. This method involves forging the material above its beta transus temperature, which results in a unique microstructure that can enhance the component's strength and fatigue resistance. Beta processing requires precise control over temperature and deformation parameters to achieve the desired properties.
Near-net-shape forging is an advanced approach that aims to produce components as close to their final dimensions as possible, minimizing the need for extensive machining. This technique requires sophisticated die design and process control but can significantly reduce material waste and production costs.
Precision forging takes the concept of near-net-shape forging even further, producing components with extremely tight tolerances and excellent surface finishes. This method often involves multiple forging steps and may incorporate isothermal forging techniques to achieve the highest level of dimensional accuracy.
Challenges and Considerations in Titanium Forging
Maintaining precise temperature control throughout the forging process is crucial for titanium alloys. Overheating can lead to excessive grain growth and property degradation, while underheating can result in poor formability and potential defects.
The design and material selection for forging dies are critical factors in titanium forging. Dies must withstand high temperatures and pressures while maintaining their shape and surface quality. Advanced materials and cooling techniques are often employed to extend die life and improve forging results.
The forging process significantly influences the microstructure of titanium alloys, which in turn affects their mechanical properties. Careful control of forging parameters, including temperature, strain rate, and deformation degree, is essential for achieving the desired microstructure and properties.
Titanium forging can be a costly process due to the high material costs, specialized equipment requirements, and energy-intensive nature of the operation. Optimizing the forging process and minimizing material waste are crucial for maintaining cost-effectiveness.
The aerospace industry is one of the largest consumers of forged titanium components. These parts are used in aircraft engines, structural components, and landing gear systems, where their high strength-to-weight ratio and excellent fatigue resistance are invaluable.
In the automotive industry, forged titanium components are increasingly being used in high-performance vehicles for parts such as connecting rods, valves, and suspension components. The lightweight and high-strength properties of titanium contribute to improved fuel efficiency and performance.
Titanium's biocompatibility and corrosion resistance make it an ideal material for medical implants. Forged titanium is used in various orthopedic and dental applications, including hip and knee replacements, bone plates, and dental implants.
Forged titanium components find use in various industrial applications, particularly in chemical processing, oil and gas extraction, and marine environments, where their corrosion resistance and strength are highly valued.
The integration of additive manufacturing techniques with traditional forging processes is an emerging trend in titanium component production. This hybrid approach combines the design flexibility of 3D printing with the superior mechanical properties achieved through forging.
Continued advancements in computer simulation and modeling techniques are enabling more accurate prediction of material behavior during forging. This allows for optimized process design and reduced development time for new components.
As environmental concerns grow, the titanium forging industry is focusing on developing more sustainable practices. This includes improving energy efficiency, reducing material waste, and exploring recycling options for titanium scrap generated during the forging process.
The titanium forging process is a complex yet crucial manufacturing technique that enables the production of high-performance components for various industries. By carefully controlling each stage of the process, from billet preparation to post-forging operations, manufacturers can harness the exceptional properties of titanium alloys to create parts that meet the most demanding requirements. As technology continues to advance, the titanium forging industry will undoubtedly see further innovations, leading to even more efficient and capable manufacturing processes.


