

Views: 288 Author: Lasting Titanium Publish Time: 2024-10-10 Origin: Site


Content Menu
● Introduction to Titanium Forging
● The Significance of Temperature in Titanium Forging
>> Understanding the Beta Transus Temperature
>> Temperature Ranges for Titanium Forging
● Effects of Forging Temperature on Titanium Properties
● Challenges in Titanium Forging Temperature Control
● Advanced Techniques in Titanium Forging
● Optimizing Forging Temperature for Specific Applications
● Future Trends in Titanium Forging Temperature Control
>> Advanced Simulation and Modeling
>> In-Situ Monitoring and Control
What Are the Optimal Forging Temperatures for Titanium and How Do They Impact Its Properties?
● Introduction to Titanium Forging
● The Significance of Temperature in Titanium Forging
>> Understanding the Beta Transus Temperature
>> Temperature Ranges for Titanium Forging
● Effects of Forging Temperature on Titanium Properties
● Challenges in Titanium Forging Temperature Control
● Advanced Techniques in Titanium Forging
● Optimizing Forging Temperature for Specific Applications
● Future Trends in Titanium Forging Temperature Control
>> Advanced Simulation and Modeling
>> In-Situ Monitoring and Control
Titanium and its alloys have become increasingly important in various industries due to their exceptional strength-to-weight ratio, corrosion resistance, and biocompatibility. One of the key processes in shaping titanium components is forging, which involves applying compressive forces to deform the metal into desired shapes. The forging temperature plays a crucial role in determining the final properties and microstructure of titanium products.
The beta transus temperature is a critical point in titanium forging. It is the temperature at which titanium undergoes a phase transformation from its low-temperature alpha phase to its high-temperature beta phase. This temperature varies depending on the specific titanium alloy composition but typically ranges between 1700°F and 1850°F (927°C to 1010°C).
Titanium forging can be categorized into two main temperature ranges:
Alpha + Beta Forging: This process occurs below the beta transus temperature, typically between 1500°F and 1750°F (816°C to 954°C). In this range, the titanium retains a mixture of alpha and beta phases.
Beta Forging: This process takes place above the beta transus temperature, usually between 1750°F and 2200°F (954°C to 1204°C). At these temperatures, the titanium is entirely in the beta phase.
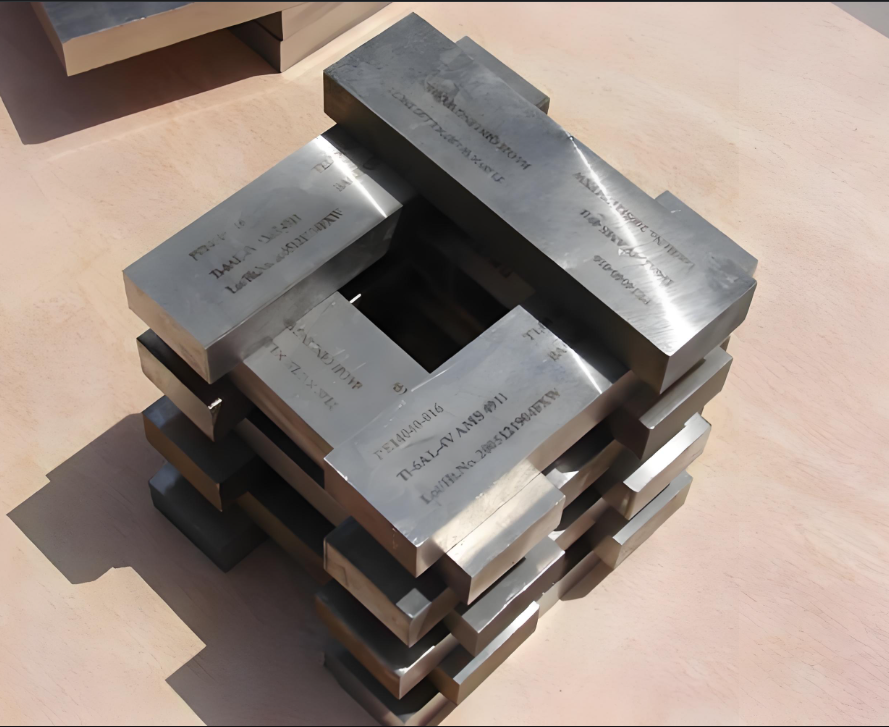
The forging temperature significantly influences the microstructure of titanium alloys. When forged in the alpha + beta range, the resulting microstructure typically consists of primary alpha grains and transformed beta regions. This structure often leads to a good balance of strength and ductility.
Beta forging, on the other hand, results in a fully beta microstructure during the forging process. Upon cooling, this structure transforms into various morphologies depending on the cooling rate and subsequent heat treatments. The resulting microstructure can range from fine, equiaxed grains to coarse, lamellar structures.
The choice of forging temperature has a profound impact on the mechanical properties of titanium components:
Strength: Generally, forging at lower temperatures within the alpha + beta range tends to produce higher strength due to the finer grain structure and higher volume fraction of the alpha phase.
Ductility: Beta forging often results in improved ductility and formability due to the more ductile nature of the beta phase at high temperatures.
Fatigue Resistance: The fatigue properties of titanium are closely linked to its microstructure. Alpha + beta forging typically yields better fatigue resistance due to the finer grain structure and more uniform distribution of phases.
Creep Resistance: Higher forging temperatures in the beta range can lead to improved creep resistance, which is beneficial for high-temperature applications.
One of the main challenges in titanium forging is the relatively narrow temperature range for optimal processing. Slight deviations from the ideal temperature can lead to significant changes in microstructure and properties. This necessitates precise temperature control throughout the forging process.
Titanium exhibits strain rate sensitivity, particularly at high temperatures. This means that the material's flow stress and deformation behavior are influenced not only by temperature but also by the rate at which it is deformed. Balancing temperature and strain rate is crucial for achieving desired properties and preventing defects.
During forging, the relatively cooler dies can cause rapid cooling of the titanium workpiece surface. This phenomenon, known as die chilling, can lead to inhomogeneous deformation and microstructure. Proper die heating and insulation strategies are essential to mitigate this effect and ensure uniform properties throughout the forged component.
Isothermal forging is an advanced technique where both the workpiece and the dies are maintained at the same elevated temperature throughout the forging process. This method allows for more uniform deformation and better control over the microstructure, especially for complex geometries.
Near-net-shape forging aims to produce components that are very close to their final dimensions, reducing the need for extensive machining. This approach often involves precise temperature control and specialized die designs to achieve the desired shape and properties while minimizing material waste.
For certain titanium alloys, superplastic forming can be employed at specific temperature ranges. This process takes advantage of the material's ability to undergo extensive plastic deformation without necking, allowing for the production of complex shapes with minimal thinning.
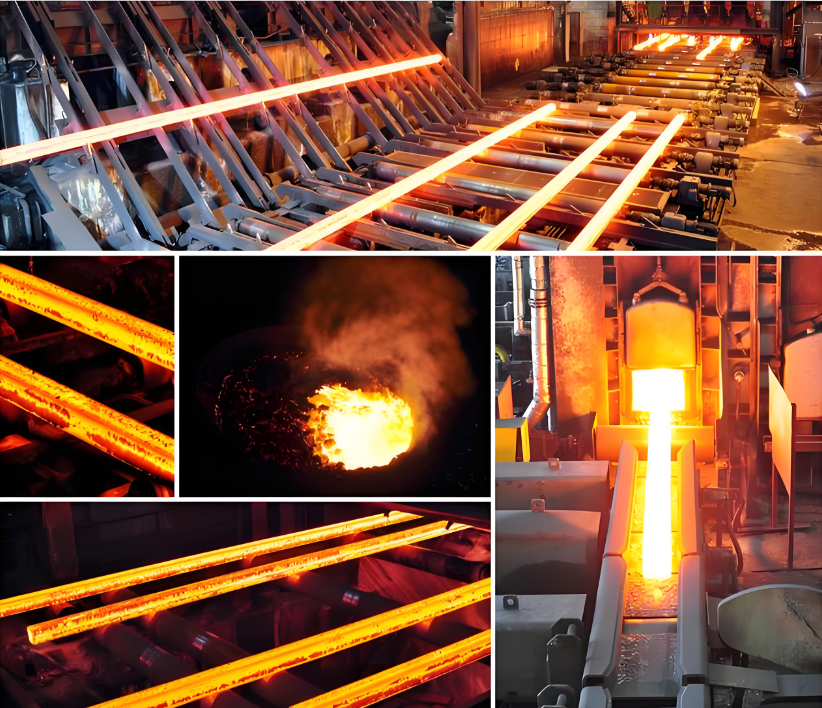
In aerospace applications, where high strength-to-weight ratio and excellent fatigue resistance are paramount, forging temperatures are often carefully selected within the alpha + beta range to achieve a fine-grained microstructure. This results in components with superior mechanical properties and long-term reliability.
For biomedical implants, the forging temperature is chosen to optimize biocompatibility, corrosion resistance, and mechanical properties. Often, a combination of alpha + beta forging followed by specific heat treatments is employed to achieve the desired balance of strength and ductility.
In marine environments, where corrosion resistance is critical, forging temperatures may be selected to promote the formation of stable oxide layers on the surface. This often involves careful control of the alpha phase content through temperature management during forging and subsequent heat treatments.
The development of sophisticated computer models and simulation tools is enabling more accurate prediction of microstructure evolution and property development during titanium forging. These advancements allow for optimized process parameters, including temperature profiles, to be determined before physical trials.
Emerging technologies for real-time monitoring of temperature and microstructure during the forging process are being developed. These systems promise to provide unprecedented control over the forging process, allowing for dynamic adjustments to maintain optimal conditions throughout the operation.
Ongoing research into new titanium alloys with improved forgability and tailored properties is likely to influence future forging practices. These developments may lead to alloys with wider processing windows or unique microstructural characteristics that can be achieved through specific temperature-controlled forging processes.
The forging temperature of titanium plays a pivotal role in determining the microstructure, mechanical properties, and overall performance of forged components. By carefully selecting and controlling the forging temperature, manufacturers can tailor the properties of titanium products to meet the specific requirements of diverse applications, from aerospace to biomedical fields.
As our understanding of titanium behavior at various temperatures continues to grow, and as advanced technologies for process control and monitoring evolve, we can expect further refinements in titanium forging practices. These advancements will undoubtedly lead to the production of titanium components with even more exceptional properties and performance characteristics, further expanding the potential applications of this remarkable metal.
The ongoing research and development in titanium forging temperature control not only promise to enhance the quality and consistency of forged products but also to improve the efficiency and sustainability of the manufacturing process. As we look to the future, the optimization of forging temperatures will remain a critical factor in pushing the boundaries of what is possible with titanium and its alloys, ensuring that this versatile metal continues to play a vital role in advancing technology across numerous industries.
Titanium and its alloys have become increasingly important in various industries due to their exceptional strength-to-weight ratio, corrosion resistance, and biocompatibility. One of the key processes in shaping titanium components is forging, which involves applying compressive forces to deform the metal into desired shapes. The forging temperature plays a crucial role in determining the final properties and microstructure of titanium products.
The beta transus temperature is a critical point in titanium forging. It is the temperature at which titanium undergoes a phase transformation from its low-temperature alpha phase to its high-temperature beta phase. This temperature varies depending on the specific titanium alloy composition but typically ranges between 1700°F and 1850°F (927°C to 1010°C).
Titanium forging can be categorized into two main temperature ranges:
Alpha + Beta Forging: This process occurs below the beta transus temperature, typically between 1500°F and 1750°F (816°C to 954°C). In this range, the titanium retains a mixture of alpha and beta phases.
Beta Forging: This process takes place above the beta transus temperature, usually between 1750°F and 2200°F (954°C to 1204°C). At these temperatures, the titanium is entirely in the beta phase.
The forging temperature significantly influences the microstructure of titanium alloys. When forged in the alpha + beta range, the resulting microstructure typically consists of primary alpha grains and transformed beta regions. This structure often leads to a good balance of strength and ductility.
Beta forging, on the other hand, results in a fully beta microstructure during the forging process. Upon cooling, this structure transforms into various morphologies depending on the cooling rate and subsequent heat treatments. The resulting microstructure can range from fine, equiaxed grains to coarse, lamellar structures.
The choice of forging temperature has a profound impact on the mechanical properties of titanium components:
Strength: Generally, forging at lower temperatures within the alpha + beta range tends to produce higher strength due to the finer grain structure and higher volume fraction of the alpha phase.
Ductility: Beta forging often results in improved ductility and formability due to the more ductile nature of the beta phase at high temperatures.
Fatigue Resistance: The fatigue properties of titanium are closely linked to its microstructure. Alpha + beta forging typically yields better fatigue resistance due to the finer grain structure and more uniform distribution of phases.
Creep Resistance: Higher forging temperatures in the beta range can lead to improved creep resistance, which is beneficial for high-temperature applications.
One of the main challenges in titanium forging is the relatively narrow temperature range for optimal processing. Slight deviations from the ideal temperature can lead to significant changes in microstructure and properties. This necessitates precise temperature control throughout the forging process.
Titanium exhibits strain rate sensitivity, particularly at high temperatures. This means that the material's flow stress and deformation behavior are influenced not only by temperature but also by the rate at which it is deformed. Balancing temperature and strain rate is crucial for achieving desired properties and preventing defects.
During forging, the relatively cooler dies can cause rapid cooling of the titanium workpiece surface. This phenomenon, known as die chilling, can lead to inhomogeneous deformation and microstructure. Proper die heating and insulation strategies are essential to mitigate this effect and ensure uniform properties throughout the forged component.
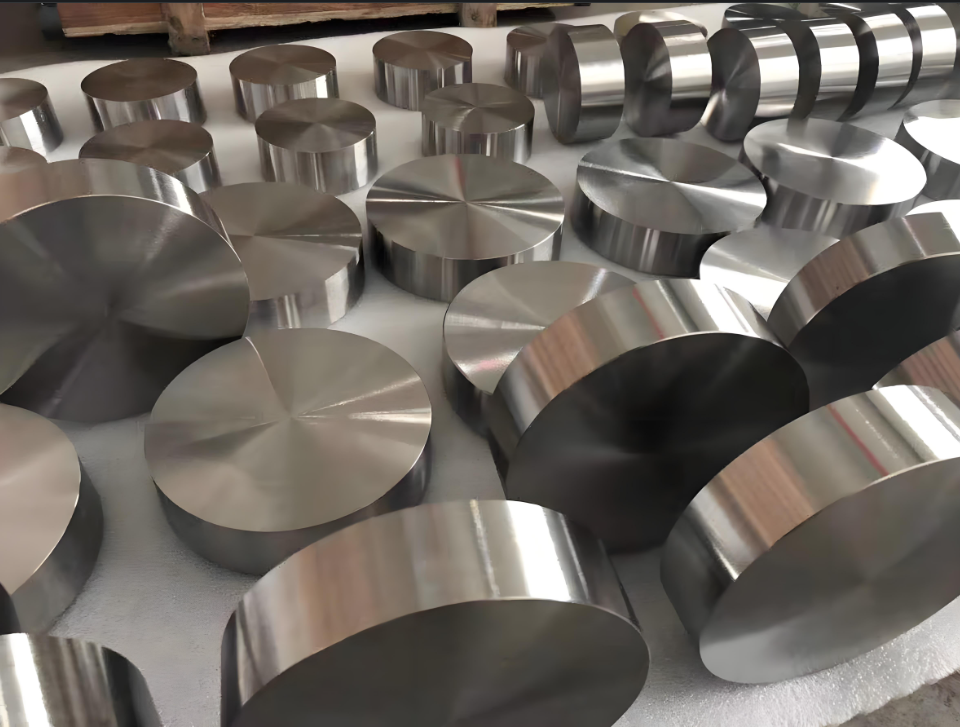
Isothermal forging is an advanced technique where both the workpiece and the dies are maintained at the same elevated temperature throughout the forging process. This method allows for more uniform deformation and better control over the microstructure, especially for complex geometries.
Near-net-shape forging aims to produce components that are very close to their final dimensions, reducing the need for extensive machining. This approach often involves precise temperature control and specialized die designs to achieve the desired shape and properties while minimizing material waste.
For certain titanium alloys, superplastic forming can be employed at specific temperature ranges. This process takes advantage of the material's ability to undergo extensive plastic deformation without necking, allowing for the production of complex shapes with minimal thinning.
In aerospace applications, where high strength-to-weight ratio and excellent fatigue resistance are paramount, forging temperatures are often carefully selected within the alpha + beta range to achieve a fine-grained microstructure. This results in components with superior mechanical properties and long-term reliability.
For biomedical implants, the forging temperature is chosen to optimize biocompatibility, corrosion resistance, and mechanical properties. Often, a combination of alpha + beta forging followed by specific heat treatments is employed to achieve the desired balance of strength and ductility.
In marine environments, where corrosion resistance is critical, forging temperatures may be selected to promote the formation of stable oxide layers on the surface. This often involves careful control of the alpha phase content through temperature management during forging and subsequent heat treatments.
The development of sophisticated computer models and simulation tools is enabling more accurate prediction of microstructure evolution and property development during titanium forging. These advancements allow for optimized process parameters, including temperature profiles, to be determined before physical trials.
Emerging technologies for real-time monitoring of temperature and microstructure during the forging process are being developed. These systems promise to provide unprecedented control over the forging process, allowing for dynamic adjustments to maintain optimal conditions throughout the operation.
Ongoing research into new titanium alloys with improved forgability and tailored properties is likely to influence future forging practices. These developments may lead to alloys with wider processing windows or unique microstructural characteristics that can be achieved through specific temperature-controlled forging processes.
The forging temperature of titanium plays a pivotal role in determining the microstructure, mechanical properties, and overall performance of forged components. By carefully selecting and controlling the forging temperature, manufacturers can tailor the properties of titanium products to meet the specific requirements of diverse applications, from aerospace to biomedical fields.
As our understanding of titanium behavior at various temperatures continues to grow, and as advanced technologies for process control and monitoring evolve, we can expect further refinements in titanium forging practices. These advancements will undoubtedly lead to the production of titanium components with even more exceptional properties and performance characteristics, further expanding the potential applications of this remarkable metal.
The ongoing research and development in titanium forging temperature control not only promise to enhance the quality and consistency of forged products but also to improve the efficiency and sustainability of the manufacturing process. As we look to the future, the optimization of forging temperatures will remain a critical factor in pushing the boundaries of what is possible with titanium and its alloys, ensuring that this versatile metal continues to play a vital role in advancing technology across numerous industries.


